
 Türkçe
 English
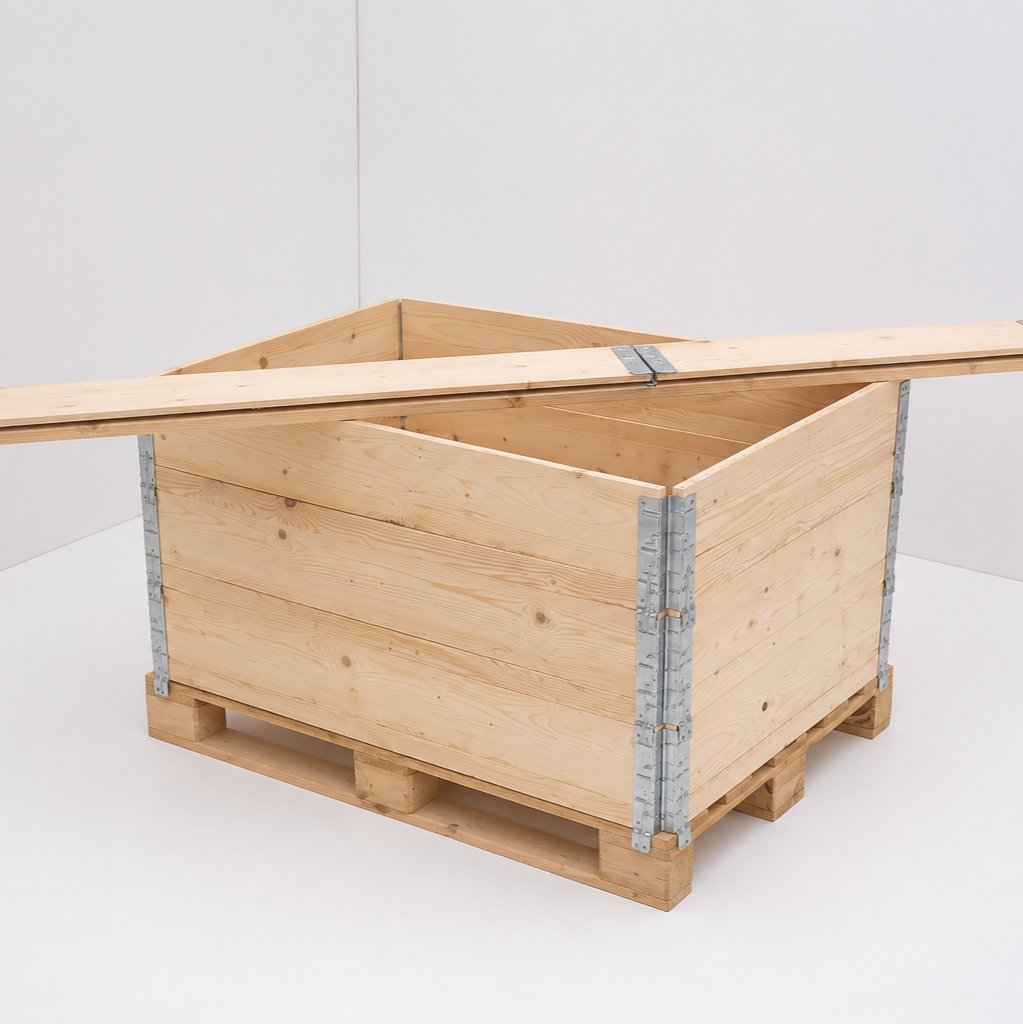
Automotive Supply Industry
Collapsible plywood crates can support recurring flows of automotive components between suppliers, assembly plants, warehouses, and service networks. Engines, gearboxes, fixtures, castings, machined components, and modules may travel in standardized packaging that folds after delivery. Compact empty returns reduce vehicle volume and storage demand where the same routes operate regularly.
Automotive parts vary significantly in weight, geometry, contact points, and sensitivity even where their external dimensions are similar. The crate base must therefore be designed from actual load transfer, while modular blocks, bolts, nests, and separators can adapt the interior to a controlled product family.
Machined surfaces, connectors, sensors, and painted parts require protection from plywood and adjacent components. Use specified interfaces, caps, sleeves, or reusable inserts. Structural restraints must stop movement independently from soft surface protection.
Line-side operations benefit from quick opening, clear identification, and predictable component orientation. Standardized labels, barcode or RFID records, retained hardware, and an assembly sequence can reduce handling time and incorrect-part delivery.
Return logistics should coordinate delivery frequency, empty-crate accumulation, folded stack limits, collection routes, and responsibility between supplier and plant. Crates that are not collected on schedule consume production-area space and weaken the business case.
Oil, grease, metal chips, and manufacturing residue can contaminate reusable packaging. Define cleaning methods and acceptable condition before each cycle. Use replaceable liners where appropriate and prevent residue from reaching panels or other components.
Crate fleets may be grouped by common footprint and capacity while using model-specific internal fixtures. This approach improves warehouse and vehicle utilization without assuming that every product can share the same restraint arrangement.
Primary Benefit in Automotive Operations
Standardized footprints, modular interiors, rapid line-side access, traceable circulation, and compact empty returns can reduce packaging and logistics cost in recurring component flows.
Before implementation, pilot the system with real products and routes. Measure packing time, part damage, folded-return density, loss rate, cleaning requirements, and completed reuse cycles. Scale only after structural and operational performance is verified.
Food and Agricultural Products
Collapsible plywood crates may support selected food-processing equipment, agricultural components, packaged goods, and non-direct-contact supply operations where compact empty storage and recurring logistics are valuable. Suitability depends on hygiene, moisture, contamination, ventilation, and regulatory requirements—not sector name alone.
Direct food contact requires a separate material and compliance assessment. Standard plywood, timber, adhesives, coatings, and hardware must not be assumed food-safe. Where food products are carried, use approved primary packaging or liners that isolate them from the crate and meet the applicable legal and customer conditions.
Moisture is critical for agricultural and food-related operations. Wet products, condensation, washdown environments, or cold-chain transitions can affect plywood edges, timber bases, hardware, and product quality. Select coatings, liners, drainage, and storage conditions for the actual exposure.
Cleaning and sanitation methods must be compatible with the crate. Excessive water, steam, aggressive chemicals, or incomplete drying may damage panels or create microbial risks. Define a validated cleaning process, inspection criteria, and maximum acceptable contamination.
Ventilation requirements vary. Some packaged agricultural goods may need airflow, while others require sealed protection against dust, pests, or moisture. A closed collapsible crate may incorporate controlled vents or carry a separately ventilated inner package where appropriate.
Traceability should link crate identity, previous contents, cleaning status, inspection date, and current load. Segregate crates by approved product group to avoid allergen, chemical, odor, or biological cross-contamination.
For exports, assess ISPM 15 for solid-wood bases, skids, and blocks, plus destination phytosanitary conditions. The plywood body does not automatically exempt solid-wood components, and field-added dunnage must follow the same controls.
Core Control for Food and Agricultural Applications
Confirm contact suitability, hygiene, moisture behavior, cleaning validation, contamination segregation, ventilation, traceability, and export requirements before approving the crate.
The strongest applications are controlled flows of packaged goods, machinery parts, tools, or processing equipment where the crate does not replace approved food-contact packaging. Conduct a risk assessment and pilot under real temperature, humidity, cleaning, and handling conditions.
Textiles and Retail
Textile and retail operations can use collapsible plywood crates for recurring distribution of garments, fabric rolls, footwear, displays, fixtures, samples, and store equipment. The folding structure reduces empty warehouse and return-vehicle volume after products are delivered.
Textiles are vulnerable to dust, moisture, odors, staining, snagging, and compression. The crate interior should be smooth, clean, dry, and free of exposed fasteners or sharp panel edges. Use liners, bags, separators, or garment-specific supports where direct contact is undesirable.
Garments and soft goods may settle or deform under stacking pressure. Internal shelves, hanging rails, dividers, or lightweight compartments can preserve presentation. Do not rely on the outer crate to prevent compression where the contents themselves are unsupported.
Fabric rolls require cradles or end supports against rolling and concentrated pressure. Long rolls may need intermediate support to avoid bending. Protect roll edges and surfaces from hardware and timber.
Retail fixtures, mannequins, and display components have irregular geometry and fragile finishes. Modular restraints, labeled compartments, and an opening sequence can reduce setup time and prevent parts from being lost between stores or events.
Closed plywood sides improve privacy and dust separation but do not guarantee moistureproofing. For long storage, seasonal inventory, or maritime routes, evaluate inner film, desiccants, ventilation, and warehouse humidity according to the products.
Return programs should define crate ownership, store collection, folding instructions, hardware retention, contamination checks, and consolidation hubs. Clear graphics can help retail staff collapse units safely without specialist tools.
Suitable Use Model in Textiles and Retail
Recurring routes, standardized store or event kits, clean internal protection, easy assembly, and reliable empty returns create the strongest operational benefit.
Compare the reusable crate with cartons and one-way wooden packaging using damage rate, presentation quality, labor, return volume, storage, loss, and completed cycles. A pilot across representative stores or routes should confirm practical savings.
Machine Parts Transport
Collapsible plywood crates can transport machine parts where a strong reusable base is combined with a folding enclosure. Pumps, motors, gearboxes, molds, fixtures, shafts, castings, and machined components may benefit from compact empty returns after delivery.
For heavy parts, the base—not the plywood walls—carries the load. Main skids, cross-members, blocks, bolts, and metal connections must transfer weight from actual contact points to forks and transport floors. External fit alone does not demonstrate capacity.
Machined surfaces should not touch timber directly. Use corrosion-compatible separators, caps, sleeves, films, or reusable nests. Prevent metal parts from colliding with one another using partitions and dedicated restraint zones.
Bolted restraint suits parts with approved holes or chassis points. Connect bolts into reinforced base members. Where drilling is prohibited, use shaped blocks, clamps, cradles, or straps that transfer forces without damaging precision surfaces.
Long shafts and cylindrical components need intermediate supports and anti-roll cradles. Offset or tall parts require center-of-gravity-aware lifting and lateral restraint. Mark gross weight and approved handling directions on the assembled crate.
Oil and machining residue can affect plywood, anti-slip performance, cleaning, and future cargo. Use drip protection or removable liners and define cleaning acceptance before reuse. Inspect for corrosion or contamination after storage.
For maritime routes, closed plywood walls do not eliminate condensation. Barrier film, desiccants, and corrosion inhibitors may be required. Sharp metal edges and projections must not puncture the barrier during repeated packing.
Suitable Crate Structure for Machine Parts
Use a weight-rated base, product-specific restraints, surface protection, correct lifting access, and a folding plywood body designed for repeated assembly.
Provide dimensions, net weight, feet, center of gravity, material, surface sensitivity, lifting method, route, and expected cycles. Verify the complete crate through a load and handling trial before recurring use.
Internal Warehouse Circulation
Within warehouses and factories, collapsible crates can circulate between empty storage, packing stations, production lines, dispatch, returns, inspection, and repair. Folding reduces congestion when empty units wait between cycles and can improve use of racks and floor positions.
Design the flow before introducing the crate fleet. Define separate routes and zones for assembled empty units, folded units, loaded crates, returned crates, inspection-pending units, repairs, and rejected packaging. Clear status control prevents unsafe crates from re-entering operation.
Assembly and folding stations require enough space for panels, lids, tools, and personnel. Ergonomic height, component weight, pinch points, sharp edges, and locking forces should be assessed. Mechanical aids may be necessary for large systems.
Standard footprints and folded heights improve rack planning. Mark safe stack quantity, orientation, empty weight, and forklift entry. Keep hardware and panels within the same identified unit to avoid mismatched assemblies.
Forklift routes must suit entry direction, fork length, load center, aisle width, and rack geometry. Operators should handle loaded and folded stacks only from approved points. Damaged channels or bases require segregation.
Inventory systems can track crate ID, size, condition, location, assigned product, cycle count, and due return. Barcode, RFID, or warehouse-management integration helps avoid unnecessary purchasing and production delays caused by missing packaging.
Balance the number of crates across the cycle. Too few units interrupt production; too many consume capital and space despite folding. Use production rate, route time, return delay, cleaning and repair lead time, and safety stock to size the fleet.
Collapsible-Crate Cycle in Warehouse Flow
Empty storage → assembly → packing → dispatch → return → folding → inspection and cleaning → approved storage or repair.
Measure travel distance, handling touches, assembly time, floor and rack positions, waiting, damage, and missing units before and after implementation. Storage savings are most valuable when the complete material flow also becomes safer and more predictable.
Reuse and Maintenance
Reuse depends on systematic inspection and maintenance, not on the crate remaining visually recognizable. Each cycle exposes the base, panels, hinges, locks, fasteners, and restraints to load, vibration, moisture, impacts, and assembly wear.
Inspect the load-bearing base for cracked or crushed skids, bent cross-members, loose joints, damaged fork channels, deformation, and contamination. The base must remain compatible with the intended product weight and contact points.
Check plywood walls and lids for cracks, delamination, swelling, broken edges, warping, punctures, and contamination. Damage near hinges, locks, and structural profiles can prevent correct assembly or reduce enclosure performance.
Operate every hinge, clip, latch, locking tab, and removable fastener. Replace bent, corroded, loose, or missing hardware with specified components. Improvised hardware may not provide the intended alignment or transport resistance.
Inspect internal blocks, bolts, straps, foam, liners, and modular fixtures for wear and product compatibility. Compressed cushioning or distorted nests may no longer protect correctly even if the outer crate remains usable.
Cleaning must match contamination and material limits. Remove oils, dust, fibers, residues, and labels without saturating plywood or damaging coatings. Dry the crate fully before folding and storage.
For export reuse, verify ISPM 15 marks, solid-wood components, repairs, and traceability. Unknown replacement timber can affect compliance. Remove misleading obsolete shipping labels while preserving required marks.
Core Checks Before Every Cycle
Verify base capacity, panel integrity, hardware operation, internal restraints, cleanliness, moisture condition, identification, and export compliance.
Record inspections, repairs, components replaced, cycle count, and retirement decisions. Defined preventive maintenance and spare-parts availability increase successful cycles and make total cost measurable.
Selecting the Right Collapsible Plywood Crate Design
Design selection must begin with the product and operating cycle, not a standard exterior size. Provide shipping-position dimensions, net weight, foot layout, center of gravity, sensitive surfaces, handling method, route, storage, return flow, and expected cycles.
Separate net product dimensions, usable internal dimensions, assembled external dimensions, and folded dimensions. Include protection, restraints, skids, lid, hardware, and folded-panel stack. These values drive product fit, container compatibility, storage, and return calculations. Select base construction for gross weight and point loads. Determine skid and cross-member sections, forklift direction, fork specifications, bolt or block locations, lifting points, and stacking capacity. The folding body must not be expected to compensate for an inadequate base.
Select plywood and body hardware for enclosure needs, cycle count, moisture exposure, assembly frequency, and repairability. Review panel thickness, grade, edge protection, profiles, hinges, locks, corrosion resistance, and replacement availability. Choose internal protection and restraints for product sensitivity. Modular fixtures suit product families only where weight and geometry remain within approved limits. Define reusable, replaceable, and single-use internal components separately.
Evaluate the complete logistics loop: packing, outbound transport, unloading, folding, empty storage, collection, return transport, inspection, cleaning, repair, and redeployment. A technically good crate may still fail commercially if one stage lacks ownership or capacity. Confirm warehouse and return-stack safety using actual folded dimensions, empty weight, contact points, rack and floor capacity, forklift access, and maximum stack height. Ensure panels and hardware are protected during reverse logistics.
For international use, define destination, customer conditions, ISPM 15 treatment and marking for solid wood, documentation, and repair controls. Also assess product-specific moisture, corrosion, hygiene, or cleanliness requirements. Build a total-cost comparison against a fixed wooden crate or other packaging, including purchase, customization, storage, outbound and return freight, labor, cleaning, inspection, repair, loss, disposal, damage, and completed reuse cycles.
Request drawings and, where risk warrants, a prototype. Test assembly, loading, restraints, forklift and crane handling, folding, stacking, transport vibration, unpacking, and return. Use the result to finalize production specifications and procedures.
Select a supplier that can support technical design, repeatable production, spare parts, repair instructions, training, traceability, and future fleet standardization. Long-term support affects service life and operational continuity.
Primary Design-Selection Criteria
Balance product fit, structural capacity, protection, folded volume, safe handling, reuse life, maintenance, return logistics, compliance, supplier support, and total cost.
The appropriate collapsible plywood crate is the design that protects the product through every shipment while repeatedly reducing empty storage and return volume under a controlled operational system.